About Non IBR Smoke Tube Boiler
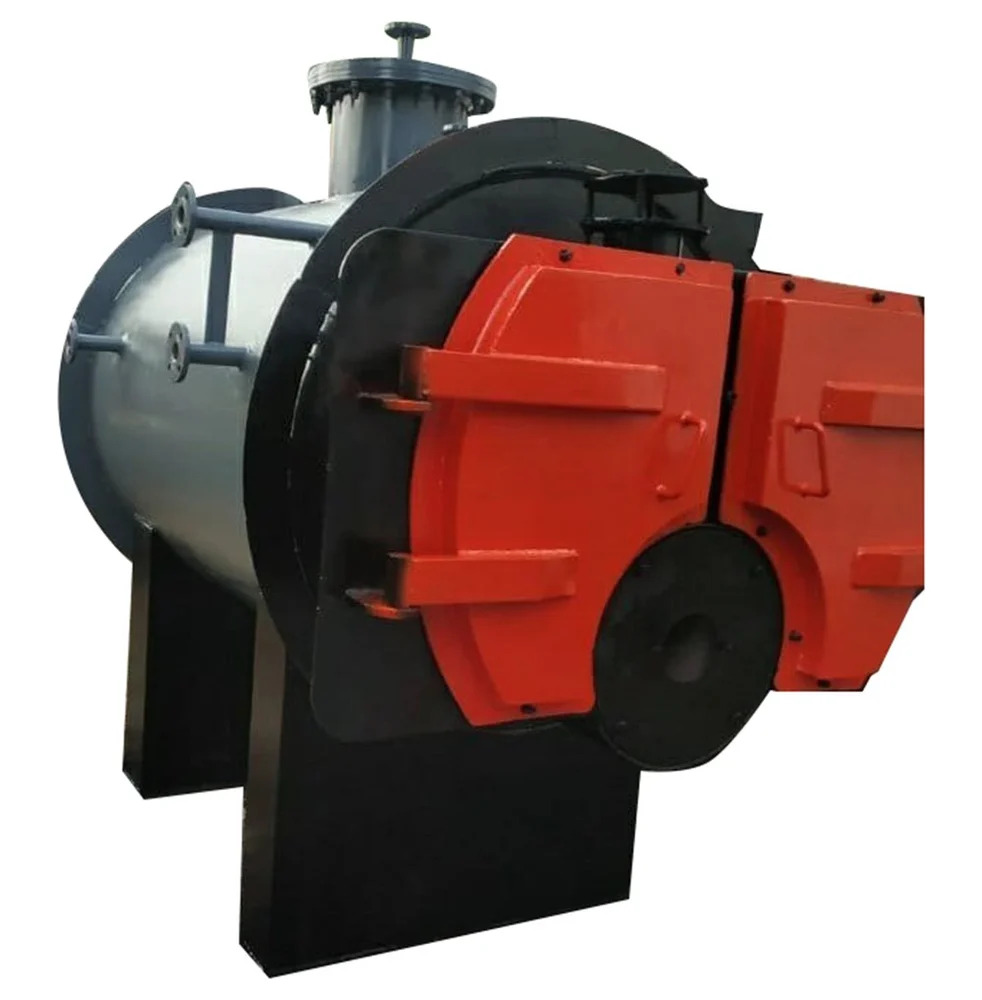
Experience affordable access to masterful steam generation with our Non IBR Smoke Tube Boiler, engineered to deliver noteworthy performance for the food and beverage industry. Boasting a ravishing red-black-gray finish and constructed from robust stainless steel, this floor-mounted, gas-fired boiler unit guarantees efficiency and reliability. Take advantage of automatic operation, a 1000 kg/hr capacity, and three-phase compatibility, making it an optimal choice for modern plants. Its cylindrical shell ensures durability, while the horizontal smoke tube design maximizes output. Proudly manufactured and supplied in India, this new boiler promises unmatched value.
Ideal Solution for Versatile Plant Applications
The Non IBR Smoke Tube Boiler stands out for its application in food and beverage processing plants, where consistent steam is essential. Take advantage of its automatic controls and robust cylindrical shell design for seamless operations. It is used as a primary steam source, delivering reliable performance for production processes. Competitive advantages include energy efficiency, low operational costs, and easy installation, making it an indispensable asset for industrial facilities seeking enhanced productivity and compliance.
Efficient Export Markets and Order Fulfillment
Arrival of your Non IBR Smoke Tube Boiler is streamlined through prompt order processing and competitive outlay. Our main export markets span across Asia, Africa, and the Middle East, ensuring international accessibility. Sample availability enables informed purchasing decisions, while the designated FOB port simplifies logistics. Each order is carefully managed for timely shipment and safe arrival, providing a reliable and transparent process for international clients seeking high-quality steam solutions.
FAQ's of Non IBR Smoke Tube Boiler:
Q: How does the Non IBR Smoke Tube Boiler generate steam efficiently?
A: The boiler operates by passing hot gases from a gas-fired burner through smoke tubes within a cylindrical shell, efficiently transferring heat to water and generating steam rapidly for industrial applications.
Q: What are the primary benefits of using this boiler in the food and beverage industry?
A: Key benefits include reliable steam output, energy-efficient operation, fully automatic controls, sturdy stainless steel construction, and compliance with food-grade requirements, ensuring seamless and safe production.
Q: Where can this Non IBR Smoke Tube Boiler be installed in a facility?
A: This floor-mounted boiler is ideal for installation in dedicated plant rooms, steam sections, or near process lines where consistent steam supply is needed for cooking, cleaning, or sterilization.
Q: When should routine maintenance be conducted on this boiler?
A: Routine maintenance should follow the manufacturer's schedule, typically monthly or as dictated by operating hours, to ensure optimal performance, longevity, and to prevent unexpected downtime.
Q: What is the process for ordering and receiving this boiler as an export?
A: Customers can request a sample, place their order, and receive timely order processing. The boiler ships from the designated FOB port with transparent logistics, ensuring smooth arrival at your location.
Q: How is the Non IBR Smoke Tube Boiler advantageous over traditional boilers?
A: Its non-IBR design offers easier compliance, faster installation, lower capital outlay, and improved automation compared to many traditional, larger industrial boilers.




 Send Inquiry


 Send Inquiry
 Send Inquiry
